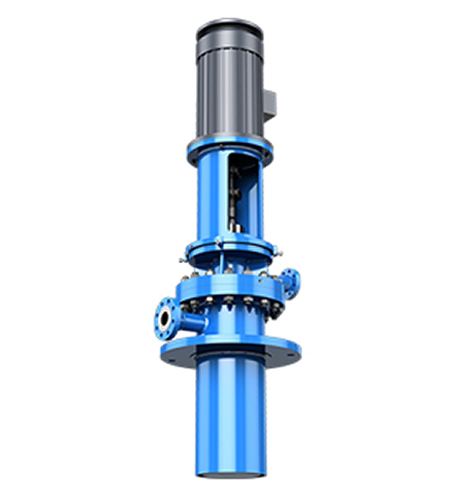
Vertical multi-stage drum bag type Canned condensate turbine pumps (barrel-type condensate pump) album
date:2026/9/25 12:18:39 source: visits:()
The Vertical multi-stage drum bag type Canned condensate turbine pump (barrel-type condensate pump) is a vertical double-layer shell industrial centrifugal pump designed specifically for high vacuum and high head working conditions. Its core advantages are excellent anti cavitation performance and easy maintenance, and it is widely used in condensate transportation fields such as thermal power and nuclear power.
🔧 Core structural characteristics of Vertical multi-stage drum bag type Canned condensate turbine pumps (barrel-type condensate pump) Double layer cylinder bag shell: The outer cylinder is welded from carbon steel or stainless steel, and maintains negative pressure inside during operation to prevent air leakage; The inner working section can be pulled out as a whole, and maintenance can be completed without dismantling the inlet and outlet water pipelines, greatly reducing downtime.
Multi stage impeller configuration: The first stage impeller adopts a single suction or double suction structure, and some models are equipped with inducers to enhance anti cavitation ability; Subsequent multi-stage impellers are arranged in series in the same direction, gradually increasing the medium pressure and achieving high head output.
Axial force balance system: More than 95% of the axial force is counteracted by the balance drum, and the residual axial force is carried by the pump body thrust bearing or motor bearing, greatly improving the operational stability.
Reliable shaft seal design: using packing seal or containerized mechanical seal, the condensed water transported by itself must be used as the sealing cooling water to avoid contaminating the system water quality. Some models comply with API682 standard.
📊 Typical performance parameters of Vertical multi-stage drum bag type Canned condensate turbine pumps (barrel-type condensate pump)parameter item
Conventional scope
Flow rate of 120-2200 m ³/h
Lift range of 36-500 meters
Medium temperature ≤ 80 ℃, special materials can reach up to 180 ℃
Rated speed 1480 r/min
The rotation direction is counterclockwise when viewed from the drive end
🏭 Main application scenarios
Thermal power plant: The vertical multi-stage drum bag type condensate turbine pump (condensate pump) is the core equipment of the 50-1000MW steam turbine generator unit, which boosts the saturated condensate water in the condenser hot well and sends it to the low-pressure heater or deaerator.
Nuclear power plant: Adapting to the strict requirements of the secondary loop system of nuclear power plants, special radiation resistant materials are used, and a Vertical multi-stage drum bag type Canned condensate turbine pump (barrel-type condensate pump) is used to ensure the long-term stable operation of the condensate recovery system.
New energy power plants: In gas steam combined cycle power plants, geothermal power plants, and concentrated solar power plants, vertical multi-stage drum bag type condensate turbine pumps (condensate pumps) are used to efficiently recover and transport high-temperature condensate water.
In the field of chemical engineering: In NPSH or chemical processes with limited installation space, vertical multi-stage drum bag type condensate turbine pumps (condensate pumps) transport clean media with physical and chemical properties similar to water, such as condensate, desalinated water, etc.
✨ Core operational advantages
Excellent anti cavitation performance: The pump body sinks into the underground wellbore and relies on water column pressure to increase the effective cavitation allowance. It can adapt to low-pressure saturated water conditions without the need for additional inducers, and its service life is extended by more than 30% compared to ordinary horizontal condensate pumps.
Efficient and energy-saving: The hydraulic model is specifically optimized for condensate water conditions, with an efficiency 2-5% higher than traditional pump types under rated conditions. A single pump in a million kilowatt thermal power unit can save hundreds of thousands of kilowatt hours of electricity per year.
Compact structure: The motor is located above and the pump body is buried underground, occupying only 1/3 to 1/2 of the floor area of a horizontal pump with the same parameters, significantly reducing the construction cost of the pump room.
Convenient maintenance: The Vertical multi-stage drum bag type Canned condensate turbine pumps (barrel-type condensate pump) adopts a core withdrawable design, and during maintenance, only the internal rotor components need to be extracted to complete the operation, reducing downtime by about 50%.
 WeChat